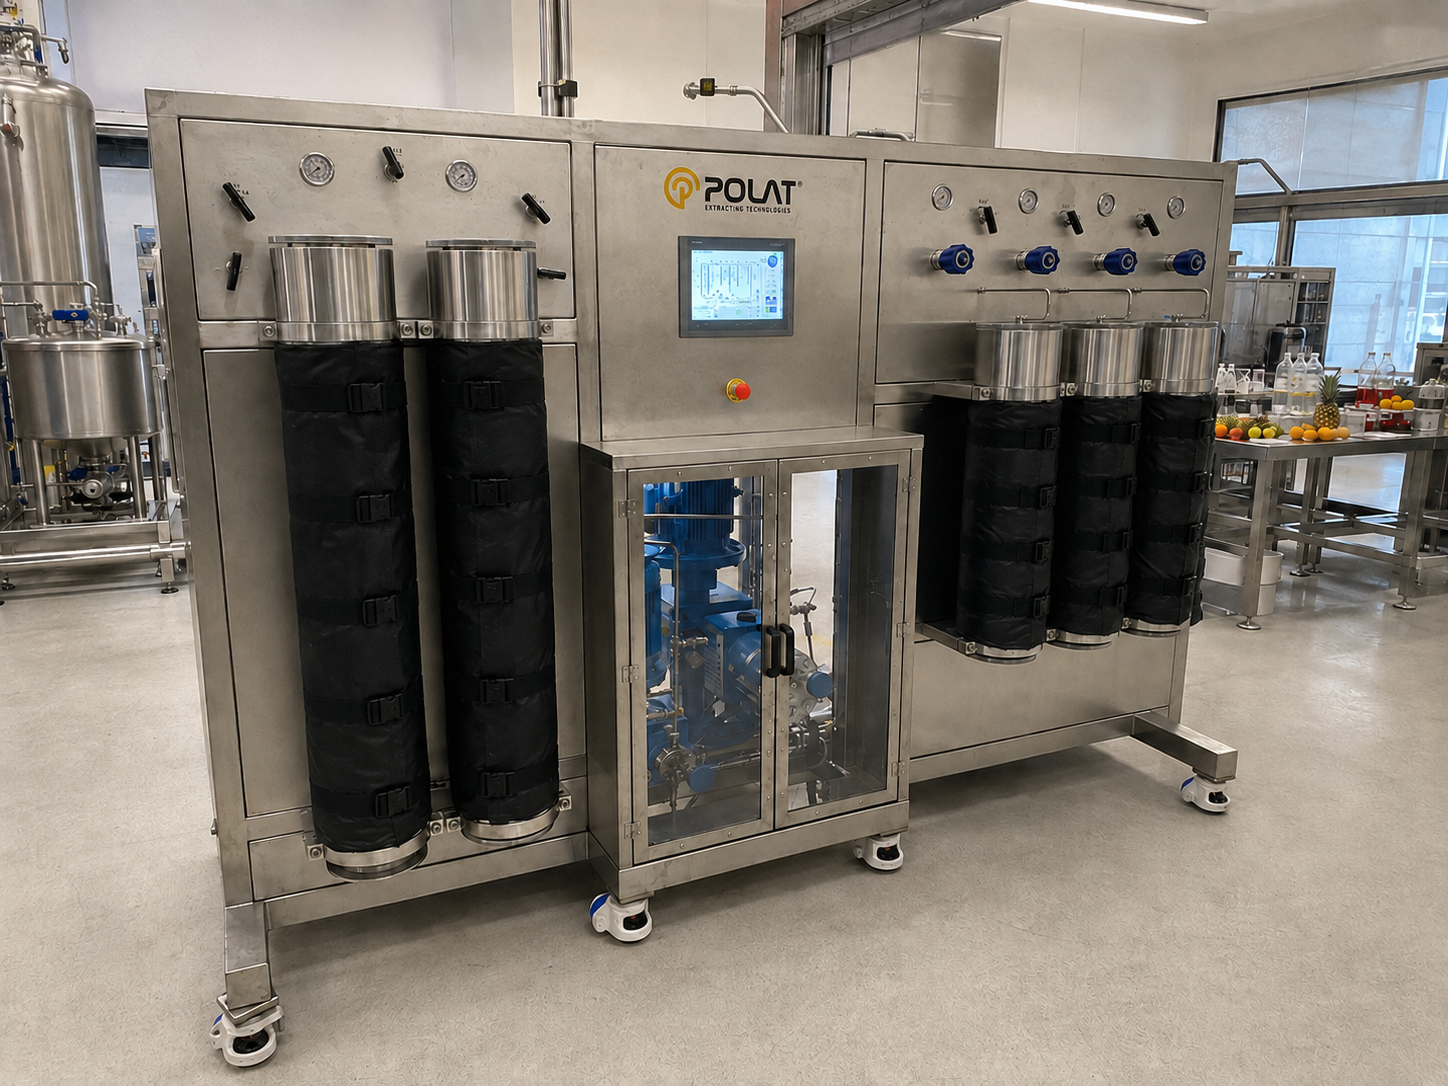
Our Supercritical Fluid Extraction (SFE) technology has been implemented at a high-tech manufacturing facility producing natural ingredients for the food and beverage industry. The system is designed to process a variety of botanical raw materials, particularly hops, fennel, and fruit seeds recovered from juice production.The primary objective of the project is to establish a flexible, highly selective extraction process that can handle different raw materials using the same process infrastructure, optimize extraction conditions according to the target compounds, and preserve heat-sensitive natural ingredients.
Technical Process and Supercritical CO₂ Extraction Engineering
Hops, fennel, and various fruit seeds require different extraction conditions depending on their oils, aroma compounds, and other valuable natural constituents. Since the solvent power of supercritical CO₂ can be adjusted through pressure and temperature, the same system can accommodate process-specific extraction recipes tailored to different raw materials and target products.
Resins, alpha acids, beta acids, and aromatic oil components found in hops can be selectively extracted using supercritical CO₂. By controlling pressure, temperature, and CO₂ flow rate, process conditions can be optimized to achieve the desired extract characteristics.
The volatile oils and characteristic aroma compounds found in fennel seeds can be recovered through supercritical CO₂ extraction at relatively low temperatures. Lower processing temperatures help reduce the risk of thermal degradation of heat-sensitive and volatile compounds.
Fruit seeds containing oil, such as grape seeds, pomegranate seeds, and similar by-products of juice production, can be valorized through SFE to obtain high-value products. Supercritical CO₂ enables the extraction of oils and lipophilic bioactive compounds from these seeds, yielding natural extracts suitable for food and nutraceutical applications.
Critical process parameters, including pressure, temperature, CO₂ flow rate, and extraction time, are precisely controlled. This allows dedicated process recipes to be developed for hops, fennel, and different fruit seeds, optimizing extraction yield, selectivity, and product characteristics.
Key Deliverables and Added Value
Flexible Process Infrastructure for Different Raw Materials
The system enables the processing of various botanical raw materials without being limited to a single product. Different processes for recovering resins and aromatic compounds from hops, essential oils from fennel, and valuable plant oils from fruit seeds can all be carried out using the same technological infrastructure.
High Selectivity and Product Quality
By precisely adjusting pressure, temperature, and CO₂ flow rate, the solvent power of CO₂ can be optimized for the target compound. This helps enhance the extraction of desired components while limiting the transfer of unwanted compounds into the extract.
Low-Temperature Extraction
Relatively low processing temperatures limit the exposure of volatile aroma compounds, particularly those found in fennel and hops, to high temperatures. This helps reduce the risk of thermal degradation and preserve the characteristic properties of the raw materials.
Sustainable Processing and Resource Recovery
Processing fruit seeds generated as by-products of juice production enables the recovery of valuable oils and lipophilic compounds. This supports the conversion of production by-products into high-value natural extracts.
Process Development and New Product Innovation
Recovering and reusing CO₂ in a closed-loop system helps reduce CO₂ consumption. By reducing the use of organic solvents in suitable applications and valorizing fruit processing by-products, the technology supports a more sustainable approach to production.