In a modern olive oil production facility aiming to process olive batches of varying varieties, maturity levels, and qualities simultaneously or with flexible scheduling,
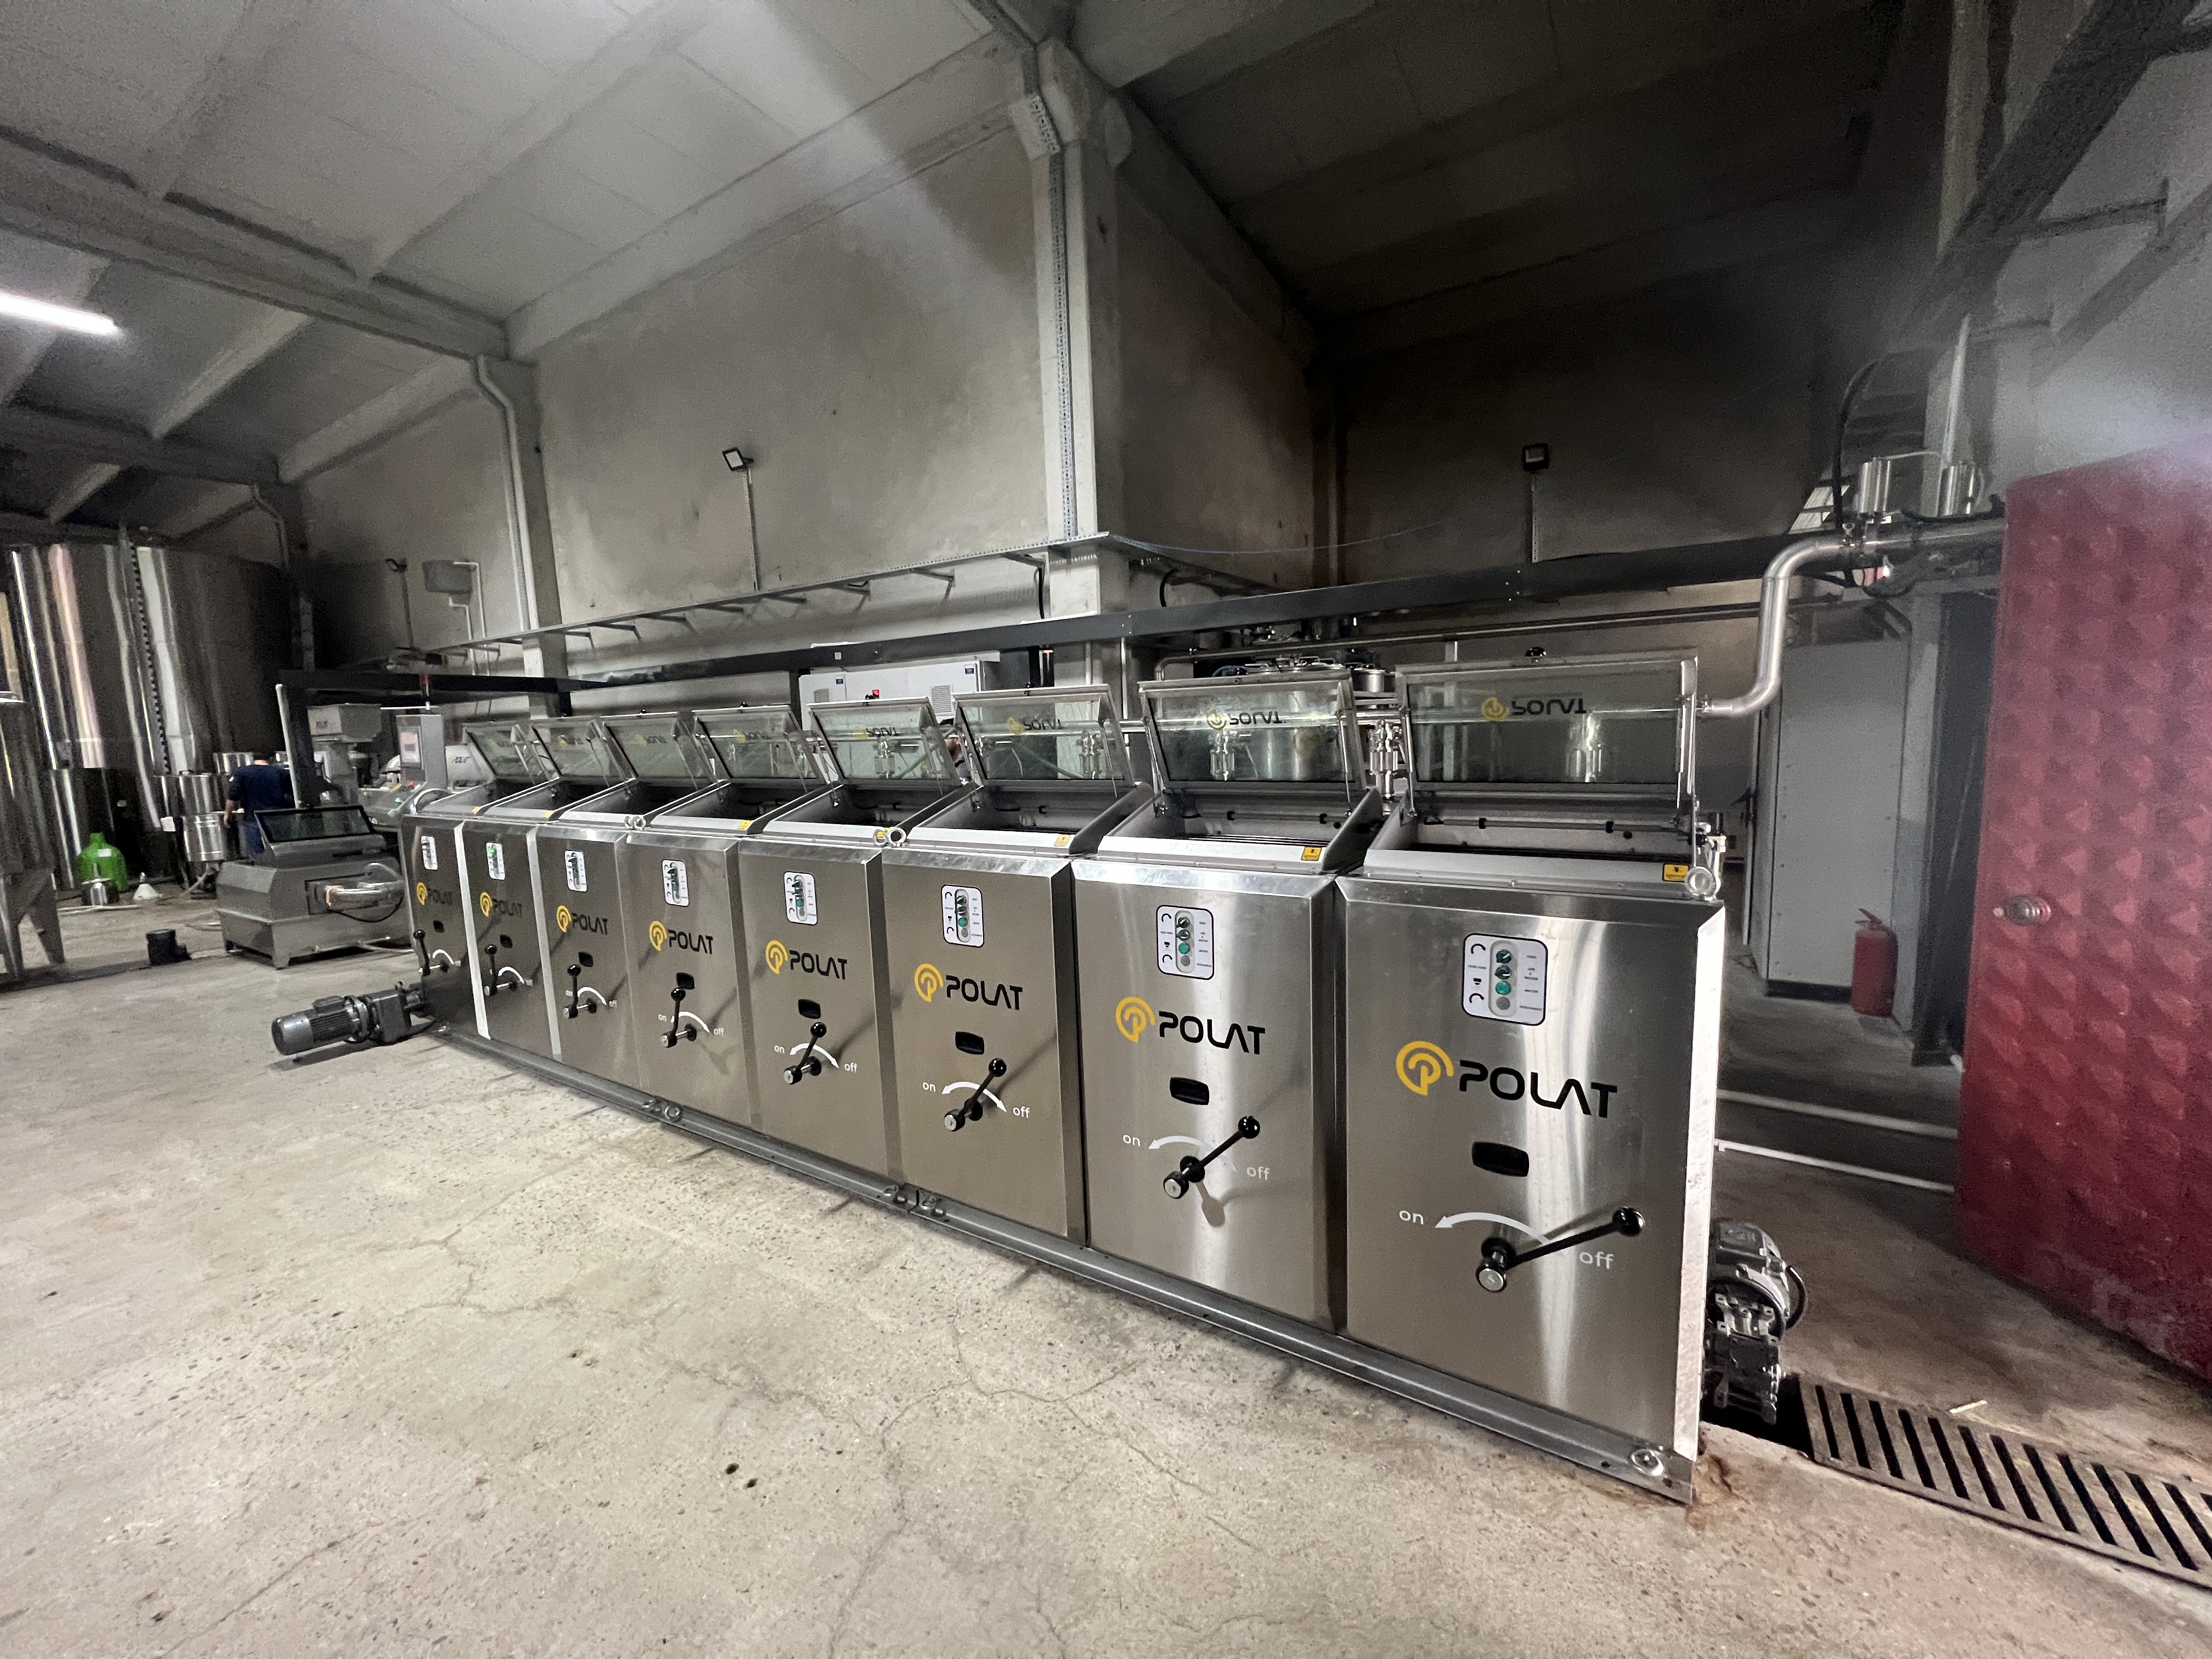
our fully modular, independent-compartment, and pneumatically controlled malaxer system has been commissioned to manage the paste preparation process with complete automation.
The main goal of the project is to ensure homogeneous maturation of the olive paste by providing independent temperature and mixing conditions in each malaxer compartment, eliminating quality errors stemming from human intervention to achieve maximum aroma and polyphenol preservation under cold-extraction standards.
Technical Process and Modular Malaxer Engineering
In olive oil extraction, processing the paste at the ideal temperature and duration directly determines the quality of the final product:
Independent Temperature and Process Management: Thanks to the fully modular structure, each malaxer compartment features an entirely independent jacket heating/cooling system. This allows low temperatures to be applied for early-harvest olives in one compartment while a different batch of olives is malaxed at its own ideal process temperature in another compartment.
Homogeneous Maturation and Specialized Blade Architecture: The specially angled agitator blade design ensures equal heat transfer to every point of the paste, enabling flawless coalescence of micro oil droplets and uniform maturation.
Pneumatic Actuated Automatic Valve Infrastructure: Pneumatically actuated valves used on paste inlet and discharge lines are fully automated via the PLC automation system. Line transitions, filling, and discharge operations occur untouched by human hands with high precision.
Full Stainless Steel Construction and Maximum Hygiene: To maintain the plant's hygiene standards at the highest level, all body, chassis, and structural components of the malaxer—both contact and non-contact with paste—are manufactured from AISI 304 / 316 grade stainless steel.
Key Deliverables and Added Value
Operational Flexibility: Olive batches coming from different growers or groves are processed at high efficiency without cross-mixing, defining customized temperature and duration parameters for each.
Prevention of Yield Loss and Quality Deterioration: Thanks to pneumatic valves and automation, paste residue between compartments and cross-contamination risks are eliminated, raising process hygiene to the highest level.
Excellent Aroma and Oil Quality: Homogeneous maturation and precise temperature control preserve volatile aromatic compounds in olive oil, preventing increases in free acidity and guaranteeing the production of premium-segment olive oil.