Maximum Quality and Efficiency: The Industry’s Highest-Capacity Decanter Technology for Fruit Processing

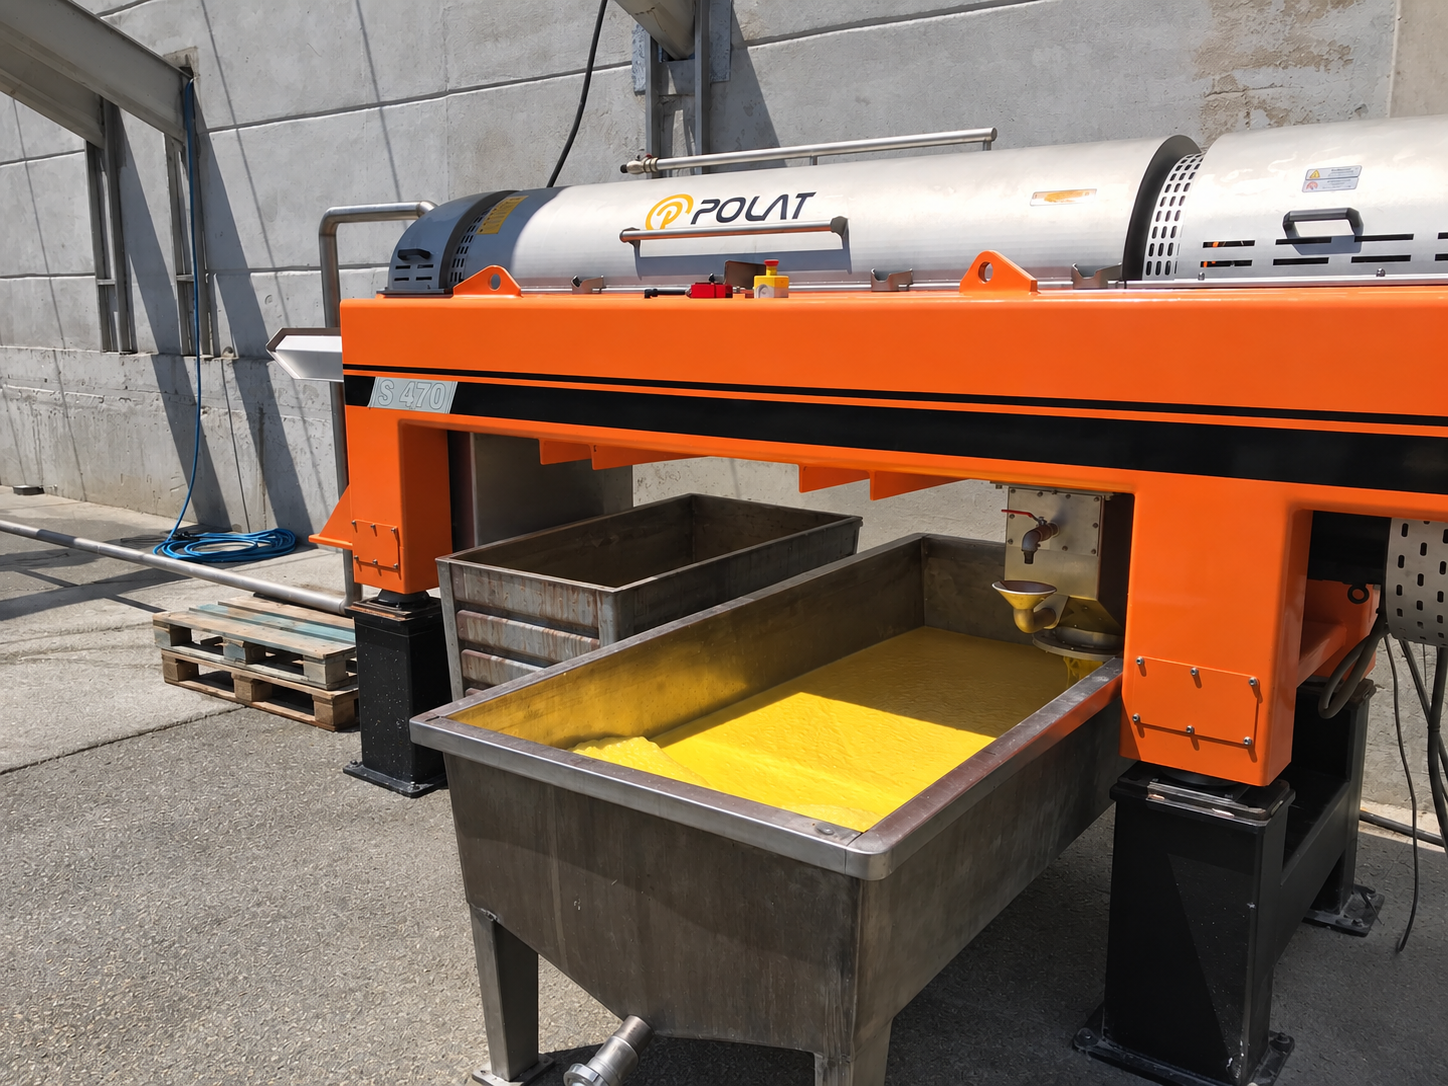
At one of Europe’s largest grape processing facilities, our advanced decanter centrifuge technology was integrated into the process to overcome the capacity and quality limitations associated with traditional screw pressing methods.

The primary objective was to produce high-purity, high-quality grape must while preserving the natural aromatic profile, freshness, and nutritional value of freshly harvested grapes.

Process and Application

In fruit processing, the complex structure of fruit mash can lead to time inefficiencies and fluctuations in product quality when conventional pressing methods are used. Our solution addresses these challenges through the following steps:

Pre-Treatment and Crushing: Fresh grapes are carefully destemmed and processed into a homogeneous mash suitable for decanter centrifugation, while preserving the characteristics of the seeds and natural sediment.

Advanced Centrifugal Separation: Instead of the mechanical pressure and lower efficiency associated with screw pressing, our high-speed, precisely controlled decanter centrifuge technology achieves highly efficient solid-liquid separation with maximum precision.

Key Deliverables and Added Value

Maximum Product Quality and Purity: Dense grape mash containing sediment, seeds, and fine particles was successfully processed to obtain high-purity grape must with the desired clarity and quality parameters.

Exceptional Processing Capacity: By deploying one of the highest-capacity machines in the industry, the project demonstrated continuous, high-throughput production performance, even during peak harvest periods.

Process Advantages Over Traditional Methods: Compared with screw presses, the solution delivers faster processing, reduced labor requirements, higher product yields, and a more hygienic processing environment.